

Industries/LNG Plant NDT Inspection
LNG Plant NDT Inspection
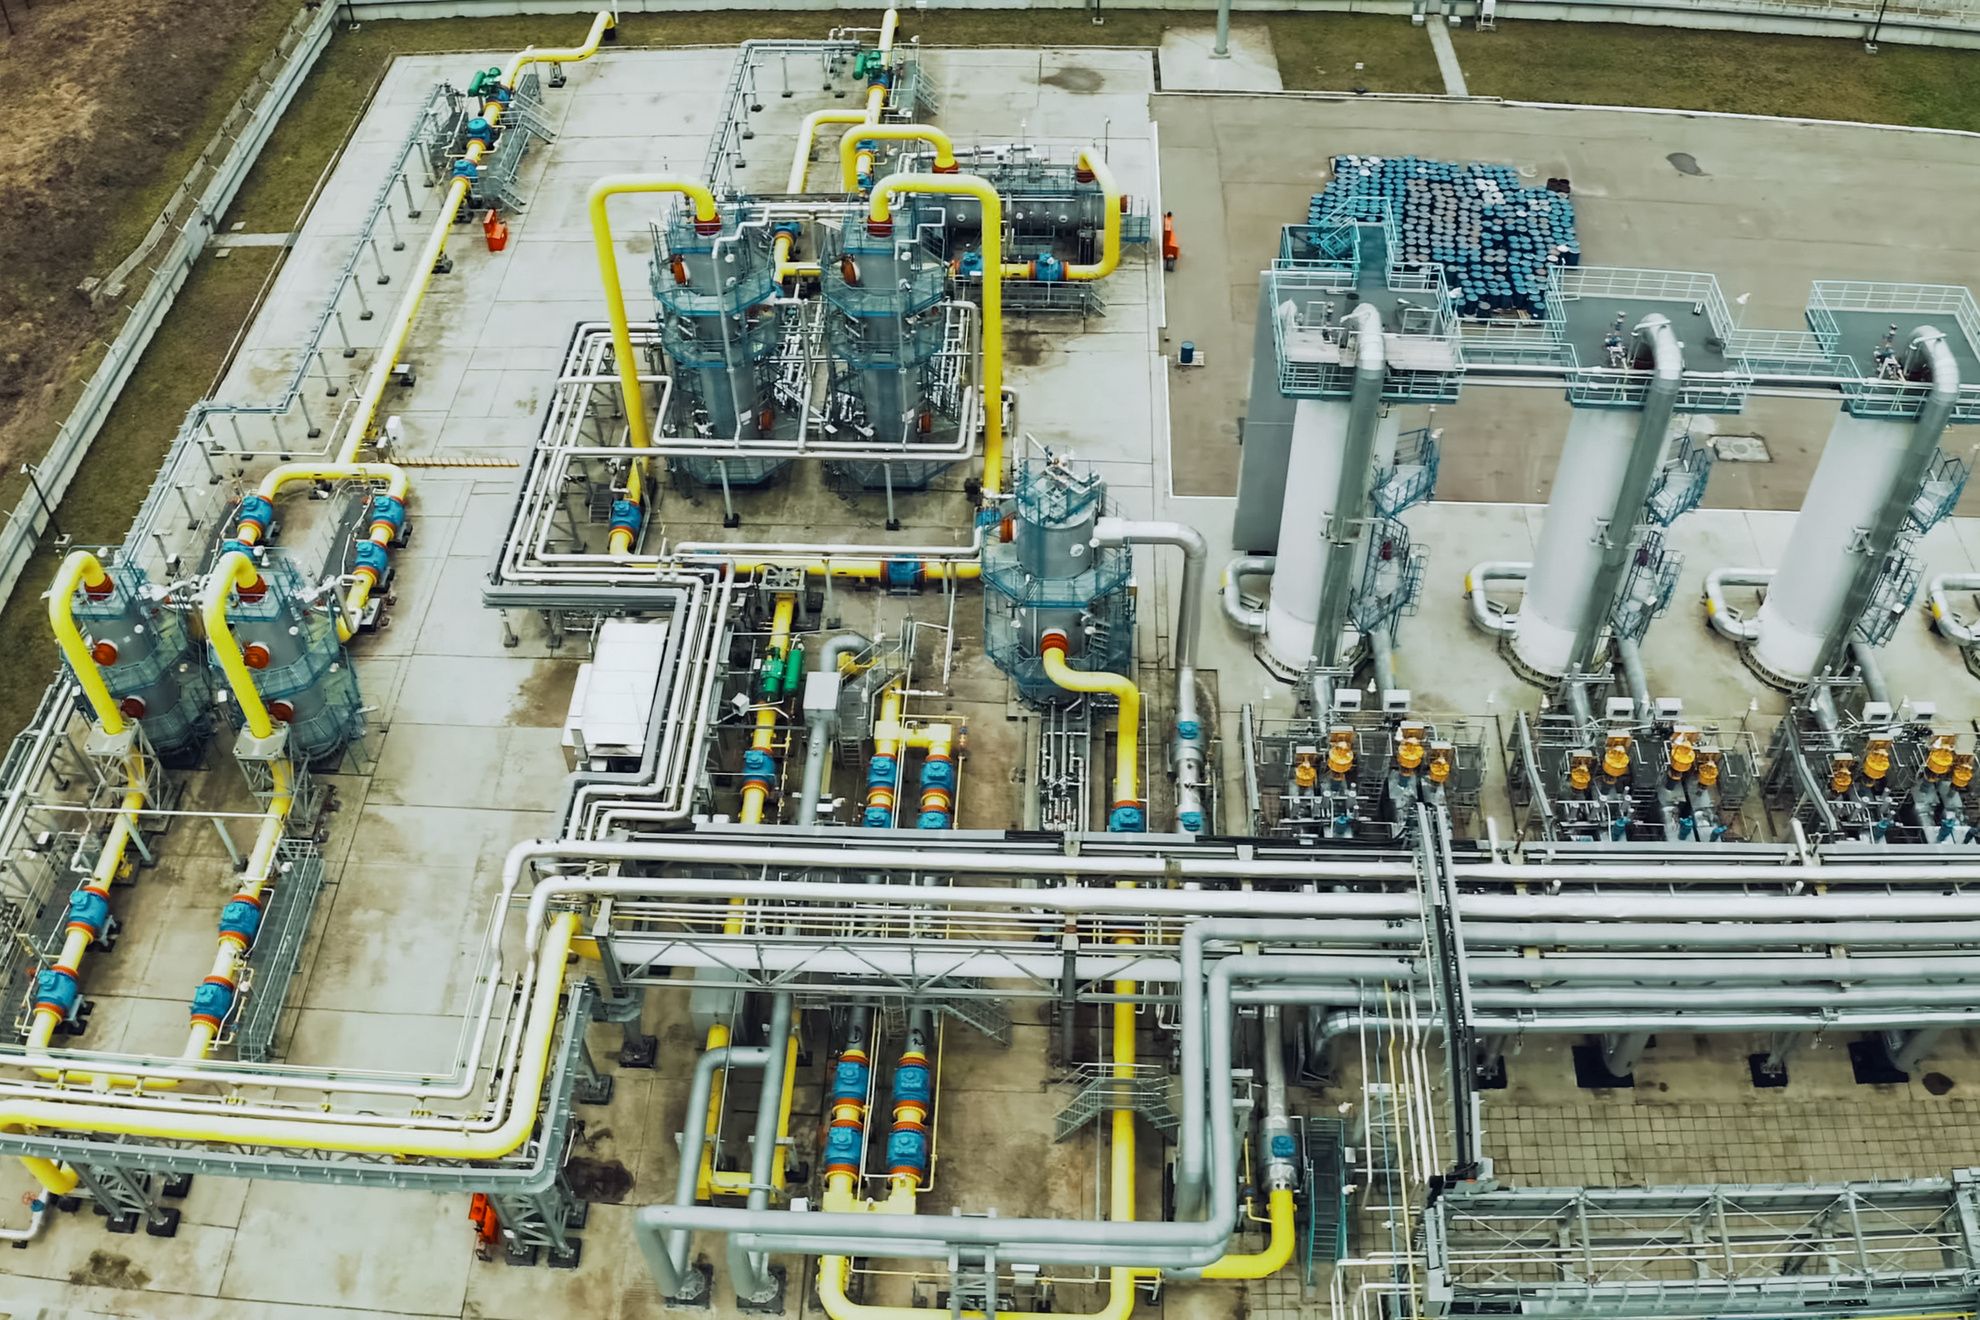
Liquefied natural gas facilities run at cryogenic temperatures — LNG is stored at about -260°F — and liquefaction and send-out systems run at high pressure, conditions where a single weld defect can halt production. Prime Inspections provides certified NDT for LNG liquefaction, regasification, and export terminal construction and maintenance — from storage tanks to loading arms.
Our Level II and Level III technicians are qualified on the UT, PAUT, RT, MT and PT techniques used on cryogenic piping, 9% nickel steel, and austenitic stainless systems, with procedures qualified to the project specification. We provide documented, code-compliant inspection reports for operator, EPC, and third-party review.
- Cryogenic Service to -260°F
- Cryogenic Piping & Tank Inspection
What we inspect
Certified Level II and Level III technicians, methods matched to the system and the governing code.
Cryogenic Storage Tanks
Full NDT inspection of LNG storage tanks including radiographic testing (RT), ultrasonic testing (UT), and magnetic particle testing (MT) on shell, annular plate, and nozzle welds — examined to the tank’s governing construction code (API 620 low-temperature annex / API 625, with NFPA 59A for the facility, as specified).
Process & Transfer Piping
PAUT, AUT, and conventional RT on cryogenic process piping, transfer lines, and regasification systems — ensuring code compliance to ASME B31.3 and API 570 standards.
Pressure Vessels & Heat Exchangers
TOFD, phased array UT, and digital radiography on LNG vaporizers, boil-off gas compressor piping, and shell-and-tube exchangers, documented against the governing construction code.
Structural & Cold-Box Inspection
MT, PT, and ultrasonic shear-wave inspection on structural steel, pipe supports, and cold-box modules subject to thermal cycling and cryogenic embrittlement risks.
LNG New Construction
Comprehensive weld inspection during greenfield and brownfield LNG construction — RT, PAUT, MT, PT, and UT on new cryogenic pipelines, tank erection, and facility expansion projects from foundation to commissioning.
Why Prime for LNG facilities
Cryogenic materials capability
Technique selection for 9% nickel steel, austenitic stainless, and the embrittlement risks unique to cryogenic service, with procedures qualified before mobilization.
Gulf Coast positioned
Headquartered in Katy, Texas, at the center of the Gulf Coast LNG build-out, with 24/7 response from offices in Katy and Lubbock, Texas plus field locations nationwide.
Code-compliant reporting
Inspection documented to ASME B31.3, API 570, and your project specification , in a format ready for operator, EPC, and regulatory review.
Advanced methods
AUT, TOFD, phased array, and digital radiography where conventional film would slow the schedule.
Related inspection services
Prime also covers these methods and industries.
Frequently asked questions
Which codes govern LNG weld inspection?
Cryogenic process piping is typically ASME B31.3; in-service piping inspection follows API 570; LNG storage tanks follow their construction code — API 620 (low-temperature annex) / API 625, with NFPA 59A governing the facility — and pressure vessels follow ASME Section VIII. We inspect and report to the governing code in your specification.
Can you support turnarounds and in-service inspection?
Yes — advanced UT methods (AUT, TOFD, PAUT) and digital radiography support both new construction and in-service integrity programs.
Do you inspect 9% nickel steel welds?
Yes — we inspect 9% nickel and austenitic stainless cryogenic systems, with the UT/PAUT technique and procedure qualified for the material before work starts, since technique selection drives both detection and schedule.
Capabilities & Technology
Put certified eyes on your welds
24/7 emergency response · Offices in Katy & Lubbock, TX + field locations nationwide · RT, DR, PAUT, AUT, TOFD, UT, MT, PT